1-Visitor
August 26, 2011
Solved

drilling issues

  • August 26, 2011
  • 36 replies
  • 10707 views

Has anyone seen this problem?

I have a part with 12 through hole and 12 counterbores on the holes. When I drill the through holes everyting works fine, But when I counter bore the holes I only get half of them. Very frustrating! No matter how I try and select them it will only cut the six holes.

After searching the knowledge base I see there is a SPR (1984609) up there addressing this issue. I will have to wait for M110 for this to get fixed.

I would think PTC could get these basic machining functions fixed and out to customers a little sooner then having to wait until the next rev. cycle on October 21.

I am running Creo/Wildfire5 M100 by the way
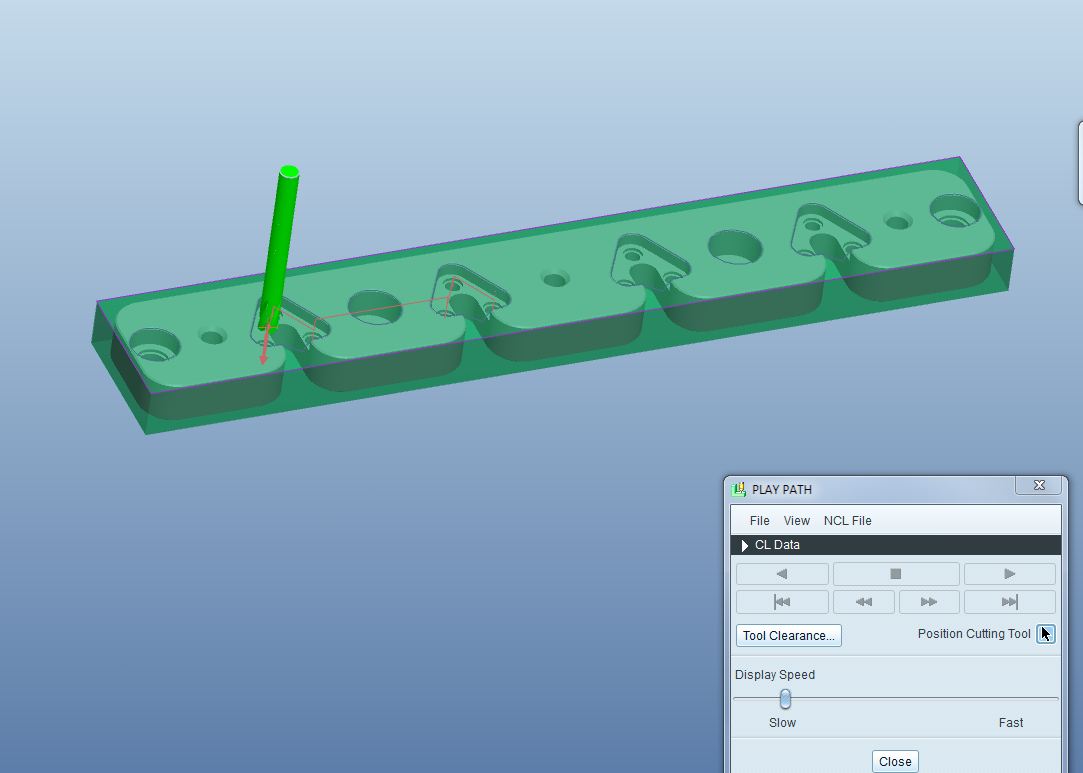
drill_issue.JPG


This thread is inactive and closed by the PTC Community Management Team. If you would like to provide a reply and re-open this thread, please notify the moderator and reference the thread. You may also use "Start a topic" button to ask a new question. Please be sure to include what version of the PTC product you are using so another community member knowledgeable about your version may be able to assist.
Best answer by BrianParrish

You could try these two option if you haven't already. Select all 12 holes and the start plane. For the depth plane try either of these two set the depth at a blind depth or create a datum plane that is specific to the hole set at the depth you require. We have seen similar issues and have been able to get around it with these two options in some instances.

And I agree that they should be able to handle basic machining without issue. The fact that we have to wait so long for a resolution to a problem only adds to our frustration.

Good luck

Brian

36 replies

12-Amethyst
August 26, 2011

That is a bad issue! Have you tried defining your counter bore sequence for three holes and then creating a refrence based pattern?

1-Visitor
August 26, 2011

Nick,

Thanks for the fast reply.

That is what I had to do. Create a pattern of the first set.

The holes were created using a mirror not sure if thats the issue or not but it is definately a bug in the software.

Best Regards,

Steve

1-Visitor
August 26, 2011

You could try these two option if you haven't already. Select all 12 holes and the start plane. For the depth plane try either of these two set the depth at a blind depth or create a datum plane that is specific to the hole set at the depth you require. We have seen similar issues and have been able to get around it with these two options in some instances.

And I agree that they should be able to handle basic machining without issue. The fact that we have to wait so long for a resolution to a problem only adds to our frustration.

Good luck

Brian

12-Amethyst
August 26, 2011

I think there needs to be more resources allocated to the manufactuing development team. I think there is posative movement in that direction and I hope to see new innovations sooner rather than later.

12-Amethyst
August 26, 2011

This has started me thinking... How can we help drive improvements? Should we open a whole bunch of enhancement requests, report bugs, or post ideas on this board? What do you guys think would help?

1-Visitor
August 26, 2011

Enhancement request seem to fall into a black hole to never be seem or heard from again. I know that PTC has been working on a new mechanism for enhancements, but this seems to be progressing at a snails pace. As it sits right now, I wouldn't waste the time to file one.

It is always a good idea to report any bugs that you find. The problem that I have ran into lately, at least for the last 6 to 9 months, is that all manufacturing support has been shipped off shore. It now seems to take days to get an SPR filed for an issue and them months to see a resolution.

Another method is to get involved with the Technical Committees.

Brian

1-Visitor
August 26, 2011

Thing that I find frustrating that I would think would be simple fixes like Being able to counter sink holes and then chamfer pockets or walls with the same tool.

Can't be done with Pro/Man you need 2 different tools cluttering your tool manager even though the tool geometry is the same.

Helical milling holes is another. It can be done, But not without a bunch of hoop jumping.

12-Amethyst
August 26, 2011

How are you milling your chamfers? I just use a custom trajectory which does allow a countersink tool to be used

1-Visitor
August 26, 2011

That is the method that we use also.

Either of you have a suggestion to get a roughing and or re-roughing to stay in the cut without jumping around like a kangaroo on steroids? We spend more time with the tool retracting and moving around to a new start location than actually making chips. Extremely frustrating for both the programmers and operators.

1-Visitor
August 26, 2011

Nick,

again you are correct you can chamfer with a countersink but you cannot countersink with a chamfer tool so I guess I need to change how I do my chamfering

Chamfer.JPG

12-Amethyst
August 26, 2011

Are you running WF5 M100? It lets me pick that tool type for custom trajectory.

New Picture.bmp

1-Visitor
August 26, 2011

Yes Nick WF5 M100

what I was saying is that I can use custom trajectory with a countersink but you cannot countersink a hole with a chamfer tool. it gives you the tool type not valid error message. Sorry for the confusion. it doesn't matter since you just showed me I can use a countersink for chamfering.

1-Visitor
August 26, 2011

Brian,

Nick posted a side milling example on here a while ago. It works great. I use it when ever I can. it works like trochoidal milling.

1-Visitor
August 26, 2011

Brian,

I know what you mean I use mill volume a lot on surfaces where i can trim to them. I works great for that. do you use a stand alone version of Vericut ? I know the pro version is very limited in it's ability. the last place I worked I had a full version and the cut optimization is nice, but expensive.

12-Amethyst
August 26, 2011

I just have the one that came with WF5. looked at switching to NC simul but couldnt justify the costs. that brings up another question when is PTC going to develope there on simulation software? And one that ties in with a stock management feature because material removal is not really that great.

1-Visitor
August 26, 2011

Another Question to everyone.

Which do you trust more gougecheck or vericut?

I do not trust vericut. and use gouge check for all my tool path checking. vericut is just a visual check of tool path and hole work because gouge check doesn't do holes. but for tight tolerance surfacing I like gouge check.

12-Amethyst
August 26, 2011

I agree with that. However gouge check does not catch tool shank interferance where as vericut does. I use both usually at the same time to limit any errors.

1-Visitor
August 26, 2011

We utilize a stand alone seats of Vericut. The shank interference is the main reason. We do a fairly sizable amount of undercutting with side milling tools.

We looked at the optimization in Vericut, but were told by CG Tech that we would need to rerun the simulation after it was optimized. This eliminated any savings that we would see. All our parts are one of's.


A quality integrated stock removal and or simulation tool is long overdue. Hopefully we will see one sometime soon.

1-Visitor
August 26, 2011

Brian,Nick,

I wouldn't hold my breath while waiting for PTC to do any verification software.

I doubt Jose reads any of this but I am sure some of the techs do.

1-Visitor
August 26, 2011

I've learnt that I wouldn't hold my breathe waiting on PTC for anything. I would have keeled over long ago.

The problem is that Jose can only work within the budget he is provided. It is the powers that be above him that control the purse strings. I know by the content at the user conference and the marketing that Windchill is the baby. Manufacturing is something that they keep around but don't really apply a great deal of development dollars too. Unlike other CAM packages that simply focus on CAM, PTC is always looking at where they get the most bang for their buck. They seem to forget that we are maintenance paying customers also.

12-Amethyst
August 26, 2011

We demand more money for Jose and his team!

1-Visitor
August 26, 2011

Brian I agree,

it's obvious where the money is. but for small companies like the one I work for it's not much fun listening to all the hype about windchill and such. it's like if you don't have 10 seat of pro and windchill you get shoved off to the side to a var like tristar and a few others for tech support. Not that there is anything wrong with that. It can be a benefit sometimes. A little more personal than going to the ptc off shore support.

1-Visitor
August 26, 2011

The company that I work for is small also, under 20 seats of Pro. We have no need for Windchill or any data management software. The life cycle on our products is relatively short. I get the feeling that we are a little more than an after thought to PTC. We have received nothing but outstanding support from our VAR, EAC, I couldn't be happier with them.

The issue that I have is when I have to deal with Tech Support. When there were engineers in the US they were knowledgeable and helpful. If there was an issue a SPR was filed within a few hours. It now takes days and the knowledge level of the support engineers seems to have diminish. They don't really seem to have any real world experience with machining. Which turns a simple issue, that should be obvious, into multiple days of back and forth before a SPR will be filed. At which point I am usually looking for a manager to talk to.

Between the lack of development dollars for the CAM product, the lack luster Tech Support, and the ever increasing complexity of machine tools that are out there we are wondering if Pro/NC is going to be the tool for the future. I know that the grass may not always be greener on the other side. But I think that is time to at least take a look. I am curious to know what it would be like to work with a CAM company that was only focused on machining. I believe that it should be an improvement or at least I can't see how it could be any worse.

Have a great weekend

Brian